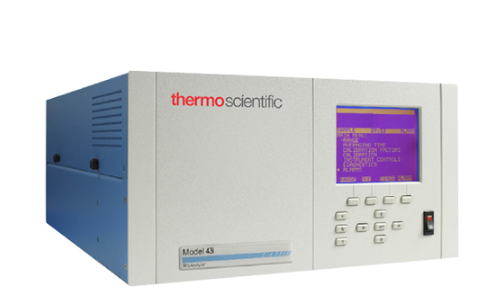
Flue gas analyzers are equipment for measuring the flue content of CO2, CO, NOx, SO2, etc., using continuous analysis of electrochemical sensors. Mainly for small-scale fuel, gas boilers or hand-held use for environmental monitoring near sources of pollution. Zhejiang Highpower Environmental will give you a brief introduction. Flue Gas Analyzers Common malfunctions and disposal methods.
Common malfunctions of analyzers and disposal methods:
I. High oxygen content that cannot be recovered
From the principles of the analyzer, it is known that O2 concentrations in the sample gas are less than 1%, and that when the gas is larger than or equal to 1%, the gas is dispersed. The oxygen analyzer used by the steel steel pellets is ABB's magnetic oxygen analyzer.
1. The flue gas lead road system is not sealed and leaked
Response: First, the main flue gas pipeline system should be examined, as the main flue gas system is being replicated, bending points and swelling more frequently, such problems should be investigated together with the corresponding mechanical staff, with gas alarms to patrol the entire channel during the rotor blow-off, with high gas or steam leaks in the pipe area, and appropriate measures should be taken to ensure that there are no leaks in the competent tunnel system.
2. Flue gas analyzer processing systems for inspection
(1) All interfaces, seals and gaskets are inspected to ensure that they are intact and in good condition;
(2) A disassembly examination of the sampling head, which, due to the high temperature of the head, contains vapour and other corrosive gases in the flue gas, can easily corrosively penetrate the inner walls of the probe, thus inhaling the outside air, resulting in a high detection oxygen content. The site is relatively secret and not easily detectable, and attention should be paid to 2-3 years of dismantling inspections;
(3) Examination of the replacement of the pump film, which must be accompanied by a certain number of spare parts, given the long and uninterrupted operation of the pump, which produces a large amount of heat and makes it easier to break up the pump film, which has a replacement period of six to eight months and is a consumer;
(4) There is a gap between the tube and the wall of the tube, where the pressure is negative, leading to the pumping of air outside the pipe, leading to the detection of high oxygen levels. If it is found that it is not in place, a tape system can be properly placed inside the drain pipe to ensure that only air does not go out, so that it can be sealed.
(5) Inspection of indoor air conditioners, which, if found to be bad air conditioners or power outages, can cause excessive indoor temperatures, thus affecting the accuracy of the analyzer and resulting in high oxygen detection;
(6) Oxygen zero drift: The analyzer, after some time in use, produces a drift of Oxygen zero, which requires regular correction of its zero point, usually once a month.
II. CONCLUSION OF THE PRESENTATION SYSTEM OF THE FASTER ANALYSIS
During routine check-ups, special attention needs to be paid to pre-pump pressure meters in the field, such as normal operations, with pre-pump pressure around -0.02bar, and if lower pressure is found, the judgment system is likely to be blocked at the site, if any, which would cause an increasing congestion, and when the pressure is less than -0.05bar, the system flow will have an alarm signal, which triggers the PLC program to stop the pump, causing the flue gas analyzer system to malfunction. As a result, routine spot checks are required to deal with anomalies in a timely manner, resulting in congestion as follows:
1. Filter jamming in sampling probes
Filters in the sample head are key components for the clean entry of the sample gas into the analyzer ' s body, since the flue gas contains a large amount of water vapour that causes moisture, so the heating of the filter must be guaranteed; furthermore, filters must be used over a long period of time and must be rebreathed in a cyclical manner, usually for a week. Finally, when purchasing filter spare parts, care should be taken to select a reasonable number, which should not be too large or too small, which can easily be too dense, with small particles covered in filter cores, blocking cores, and too small to cause a large amount of dust to enter the analyzer system, blocking the analyzer system or making measurements inaccurate. Therefore, it is generally desirable to opt for 30-35, which should have a filtering precision of 590-500um.
2. Sampling tube congestion
When the tube is used for a longer period of time, the amount of dust within the tube accumulates, resulting in a blockage of the sampling tube. At this point, when the sampling head is clogged, it can be confirmed that the sampling tube is clogged and that it can be stopped with a tropical power source, then watered into the sampling tube, and then quenched with intermediate pressure nitrogen gas for 10 minutes.
iii. Condensation failure
The cooling in the flue gas analyzer is essential, and internal detection sensors in the analyzer are never allowed into the water. Following heating of the sample head and strip to about 180°C, the sample cooled rapidly to 3-5°C through the first and second-stage condensation devices to remove the moisture from the sample. A general analyzer with an export temperature of about 4.5, and if a sample internal water is found to exist, the temperature can be set by control of a secondary analyzer with an appropriate downward adjustment of about 1°C to remove the sample water from the sample.
IV. Pump failure
We know that the flue gas analyzer is not able to enter water, and that the ingestion directly leads to damage to the analyzer's body, and therefore the creeping pump is a very important part of the system's water removal. When the creep pump is used for a certain period of time, there will be a scene where the rubber hose of the creep pump is broken, worn, or the electric card is blocked, which will prevent the discharge of the condensation water in the condensation device, such as if the gas pump continues to function and the gas analyzer’s body is damaged. Therefore, the routine check is to follow closely the condition of the rubber hose of the creep pump to see if it is broken and the rodent is intact, if there is any acoustic noise on the electric power, such as the direct replacement of the worm pump in the case described above.
Flue gas analyzer malfunctions
It is common practice to restart the analyzer’s body or to replace the internal sensor’s body.
After a certain period of time, the flue gas analyzer itself is required to perform periodic verification of the analyzer with a standard gas, for the purpose of precision testing, which is usually a one-month cycle. In addition, as the normal operation of the second steel transformer is linked directly to the ability of the transformer to blow-off, the short signal may be removed as soon as the failure is resumed, if, in a fairly urgent case, the smoke analyzer system has malfunctioned and if the transformer has to blow-out, it can be processed temporarily in the PLC blow-out conditions and production in the event of an emergency has been met.